Introduction: A successful electronic product requires more than a schematic. It needs rigorous layout, stack-up planning, routing, and a seamless transition to manufacturing. This guide covers the seven core stages of the PCB design workflow—from requirements analysis and schematic capture to layout, routing, DRC, and fabrication outputs—plus outsourcing best practices and DFM review.
Description: Based on AnyPCBA's small-to-medium volume PCB and PCBA manufacturing experience, this guide explains the complete PCB design workflow—from concept and schematic to layout, routing, file output, and DFM review—and how to ensure designs are manufacturable before production.
PCB (Printed Circuit Board) design is one of the most critical steps in electronic product manufacturing. Bringing a board from concept to reality is never just about "connecting the dots." It involves a deep interplay of electrical logic, physical layout, thermodynamics, electromagnetic compatibility, and manufacturing processes.
Many engineers create a "perfect" board in software, only to encounter a yield disaster at the factory. A mature electronic product must go through a rigorous design workflow and be seamlessly integrated with backend manufacturing.
This article systematically outlines the complete PCB design workflow from an engineering perspective and explores how to turn design intent into a manufacturable PCBA product.
The standard PCB design workflow is an evolution from the abstract to the concrete, and from logic to physical reality.
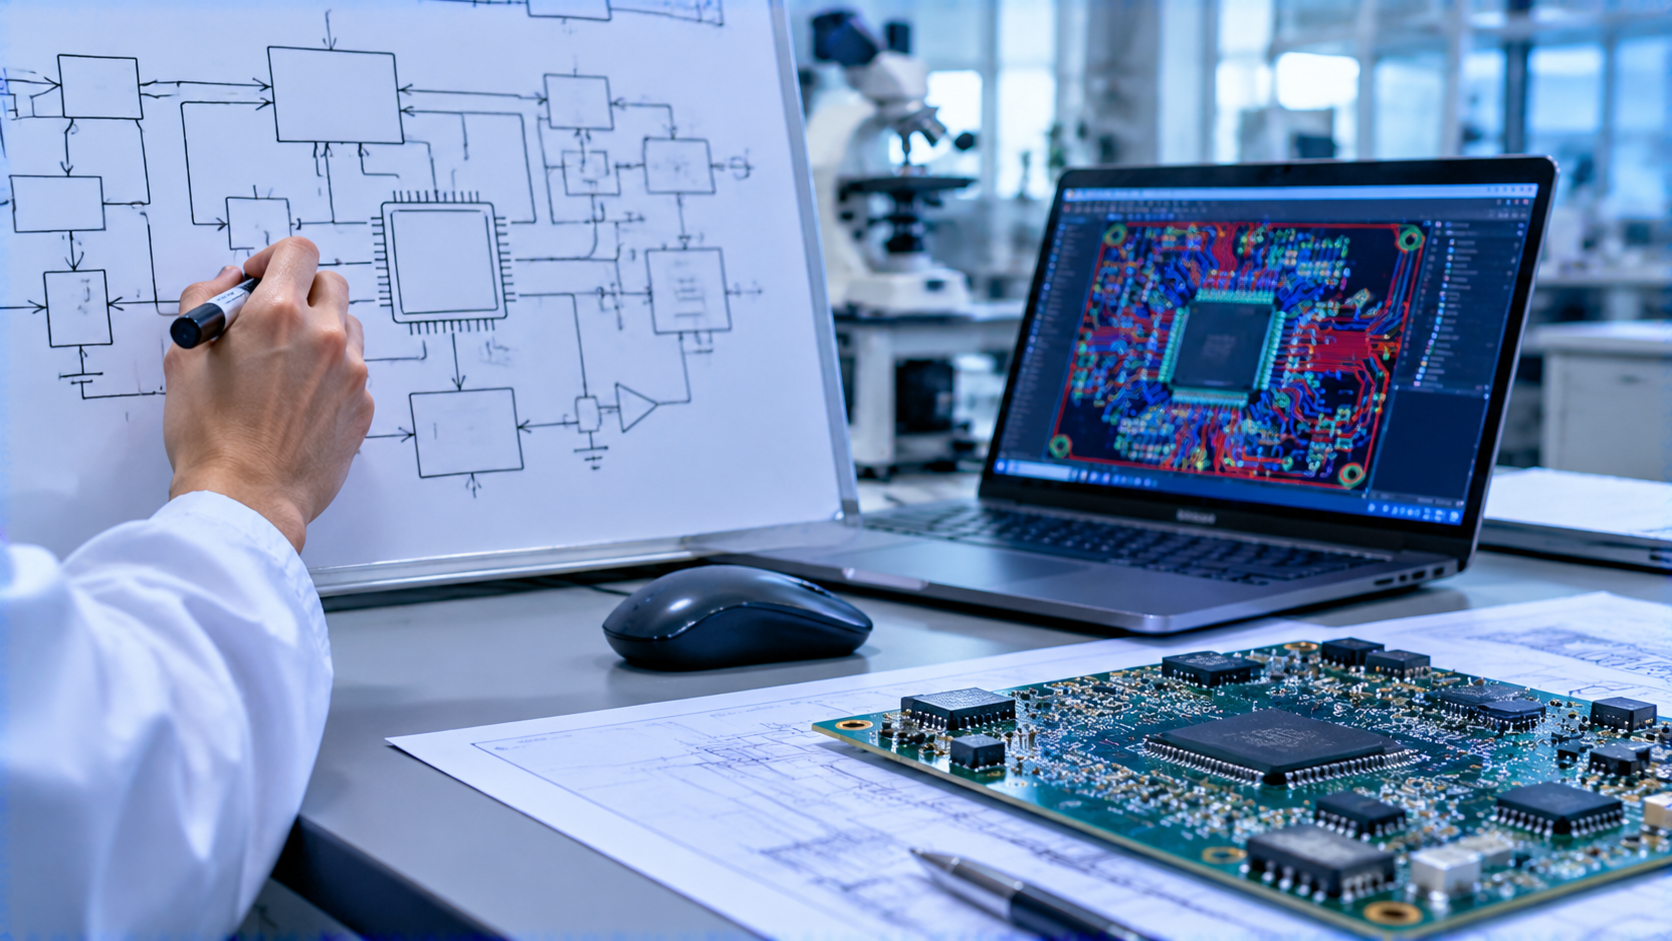
This stage determines the product's "skeleton." Engineers define the board's function, performance metrics (signal rate, power), size constraints, power requirements, and operating environment (wide temperature, vibration, EMC).
Key actions: Draw the system block diagram, evaluate the main chip and peripheral module selection, create the initial BOM (Bill of Materials) framework, and assess component lead times.
Translate the system block diagram into electronic language. Use EDA software (Altium Designer, KiCad, Cadence, etc.) to draw the logical circuit diagram.
Documentation: Beyond the complete schematic, prepare the footprint library, mechanical DXF files (connector positions and height constraints), and critical component datasheets.
Design pain point: A wrong footprint (e.g., reversed pin order) makes even the best layout useless. Building a company-standard library is essential.
After importing the netlist into the PCB software, physical placement begins. This stage determines 70% of the board's performance.
Placement principles: Large components first, then small; core components first, then peripherals. Place connectors and the main controller first, arranging them along the signal flow (straight or L-shaped) to shorten critical signal paths.
Power and ground planning: Define the power tree in advance, clarify current flow and magnitude, and design a proper GND plane for low-impedance return paths. Also consider thermal design (placing heat-generating chips near board edges or adding thermal pads).
This step is often overlooked by beginners but highly valued by experienced engineers.
Stack-up design: Determine PCB layer count, dielectric thickness, and copper weight based on routing density and impedance requirements. For example, a 4-layer board with high-speed signals typically uses a symmetrical Sig-GND-PWR-Sig structure.
Rule setup: Define classes (power, differential pairs, etc.) in the EDA software, and set strict DRC rules for trace width, spacing, and vias to support automated checking.
Routing priority: Route critical signals first (high-speed differential pairs, clocks, sensitive analog lines), then general signals, and finally power traces.
Length matching and impedance: Perform length matching for parallel buses with strict timing requirements (such as DDR), and ensure differential impedance matching for high-speed serial signals (PCIe, USB).
Power handling: Use large copper pours instead of traces for high-current areas. Critical signal traces must never cross a plane split, which can cause severe EMI issues.
DRC check: Software checks are only the baseline; manual review is essential. Look for opens, shorts, or missed rules.
Silkscreen: Place reference designators, polarity markings (diode direction, chip pin 1), version numbers, and company logos properly. Clear silkscreen greatly reduces assembly and repair difficulty.
The final design step—and the starting point of the handoff to the factory.
Gerber and NC drill files: Provided to the PCB fabricator for bare board production.
Pick-and-Place and BOM: Provided to the SMT assembler for placement and component sourcing.
Assembly drawing: Helps the factory confirm component orientation and polarity, especially for connectors and odd-form components.
Many companies—especially startups lacking an in-house hardware team—choose to outsource PCB design. This brings clear advantages: professional expertise, lower internal labor costs, and faster development.
But outsourcing is never "hands-off." To avoid a runaway project, prepare and provide these core documents:
Project requirements document: Clear functional definitions, technical specifications, environmental requirements, and expected certification standards.
Schematic and BOM: Or a clear component selection list for the design house.
Mechanical files: Accurate board outline DXF, key interface positions, and height-constrained areas.
Special process requirements: Impedance control, heavy copper, blind/buried vias, special materials, etc.
Project management matters: Set up regular meetings, define milestones, and actively participate in schematic and layout reviews. Don't wait until the board is built to discover a functional issue.
At AnyPCBA, we frequently see a painful phenomenon: many designs are perfect in software—zero red DRC errors—but impossible to manufacture at the factory.
The true PCB design workflow absolutely should not end when the Gerber files are output. The real endpoint is when the product runs smoothly on the SMT line with a yield above 99%.
Therefore, before sending your design to the factory, you must add a DFM (Design for Manufacturing) review stage:
Trace width and spacing: Confirm whether minimum trace width/spacing sits right at the factory's etching capability limit, which can cause a yield collapse.
Vias and pads: Confirm whether thermal vias under BGAs are explicitly specified for "resin plugging" to avoid solder wicking and cold joints during reflow.
Panelization and rails: Confirm whether there is enough space for the pick-and-place machine's rail transport, and whether depanelization stress will crack edge capacitors.
Impedance and stack-up: Can the factory provide the impedance control you require? Confirm the actual stack-up with the factory to ensure simulation results become reality.
AnyPCBA's engineering team performs strict DFM review before production. If we identify these risks in your files, we flag them directly and provide modification suggestions—saving you from wasting money.
After design is complete and manufacturability is confirmed, archive all project documentation. This is not only the closure of R&D, but also the key to protecting intellectual property.
Standard archiving should include:
ASM folder: Top and bottom assembly drawings
CAM folder: Gerber files, IPC netlist, production notes
DXF folder: Mechanical files
PCB and SCH folders: Final PCB and schematic source files
SMT folder: Pick-and-Place files and stencil files
Whether you design in-house or outsource, AnyPCBA provides high-quality PCB and PCBA manufacturing from prototyping to small-to-medium volume (5–5,000 pieces). We support 2 to 64 layers, including HDI, rigid-flex, and high-frequency hybrid, and hold ISO 13485 and IATF 16949 certifications. If you need professional DFM review, or want to learn more about manufacturing requirements, contact us through our website.